EN 15512
European Structural Standard
Up to 5,000 kg
Per Beam Level Capacity
ISO 9001 / CE
Certified Factory Output
+40% Density
Back-to-Back Configuration
Precision Manufacturing Catalog
High-Efficiency Pallet Racking & Specialized Storage Configurations
Direct manufacturer supply for selective pallet racks, dynamic roller systems, AGV automated bays, and cantilever superstructures tailored for GCC operational challenges.
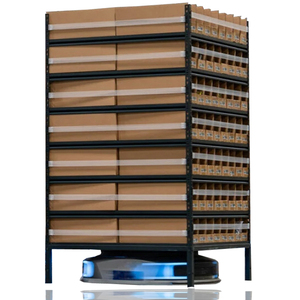
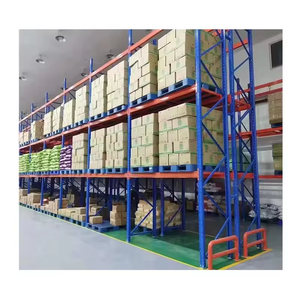
Fully Adjustable Modular Bays
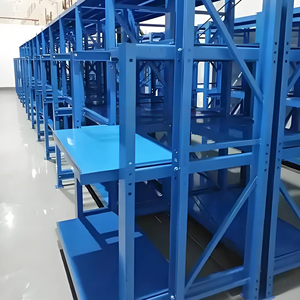
Customized Factory Warehouse Adjustable Racks Industrial Storage Shelving Supply Racking Pallet Storage Rack
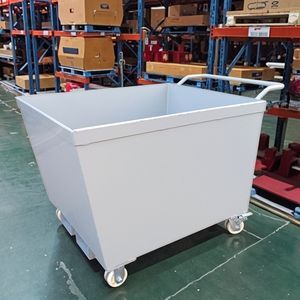
Containerization & Wire Decking
CASE CARTER OEM 600*400*400mm Heavy Duty Foldable Stack Wire Mesh Steel Pallet Storage Container Rack 4 High
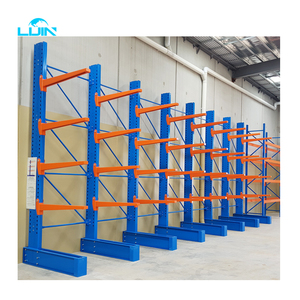
Heavy Cantilever Bar Stock
Factory Price Cantilever Rack Heavy Duty Industrial Cantilever Racking Steel Storage
Whitepaper & Technical Analysis
Engineering Back-to-Back Pallet Racking for Kuwait’s Logistical Realities
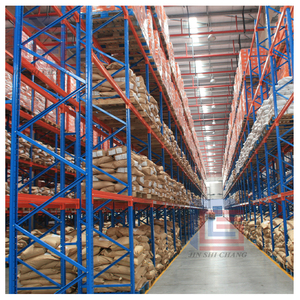
Back-to-back selective pallet racking is the standard infrastructure in modern supply chain warehousing. By placing two continuous single-entry racking rows back-to-back, connected by calibrated heavy-duty row spacers, warehouse operators eliminate duplicate transit aisles. This immediately recovers up to 40% of aisle dead space while maintaining 100% direct selectivity to each pallet position.
However, engineering industrial storage systems destined for Kuwait requires deeper consideration than standard European or East Asian baseline models. Facilities located in industrial zones like Shuwaikh, Sulaibiya, Sabhan, and the Shuaiba / Mina Abdulla oil and gas corridor operate under extreme climatic stress. Ambient summer temperatures regularly exceed 50°C, accompanied by marine-induced coastal humidity and high airborne saline sand particulate levels.
"In extreme Gulf operating environments, standard electrostatic powder coating fails prematurely due to micro-fissuring caused by thermal cycling. High-durability thermosetting polyester resins applied over multi-stage zinc phosphate pre-treatment are mandatory to maintain load integrity over multi-decade lifespans."
Our manufacturing protocols incorporate EN 10025 certified structural steels (S355JR and cold-formed high-tensile Q235B/Q355B coils), engineered strictly in accordance with EN 15512:2020 structural execution norms. We calculate seismic actions according to the Kuwait National Building Code (KNBC) and evaluate torsional upright resistance under continuous forklift impact factors, delivering unyielding reliability to Kuwait’s pharmaceutical distribution centers, food security cold facilities, and 3PL freight networks.
Technical Engineering Benchmarks
| Design Standard | EN 15512:2020 / FEM 10.2.02 / RMI Spec |
|---|---|
| Raw Material Grade | High-Yield Cold-Formed Q355B / S355JR Steel |
| Upright Frame Width | 80mm, 90mm, 100mm, 120mm, 140mm Profiles |
| Row Spacer Clearance | 200mm – 450mm (Includes Flue Space Safety) |
| Corrosion Treatment | Polyester Powder Coat (70-90μm) / HDG Galvanized |
| Floor Slab Anchoring | M12 – M16 Heavy-Duty Chemical / Wedge Anchors |
Industrial Footprint
Localized Applications Across Kuwait's Core Economic Corridors
Targeted racking system deployments engineered for distinct sector requirements, temperature limits, and warehouse heights across Kuwait Governorate hubs.
Cold Chain & Food Security (Sulaibiya)
Specialized low-temperature steel chemistry down to -30°C prevents cold-shortness embrittlement. Back-to-back designs ensure maximum cubic density in costly refrigerated environments without sacrificing lot traceability.
Pharmaceuticals & FMCG (Shuwaikh & Rai)
Strict MOH and GMP compliance demands 100% pallet selectivity and zero inventory dead zones. Back-to-back configurations provide clean floor lines, seamless integration with wire mesh decks, and unobstructed flue spaces for fire sprinkler arrays.
Oilfield & Heavy Engineering (Ahmadi / Shuaiba)
High-load configurations supporting up to 4,500 kg per bay level to store drilling valves, subsea tooling, and industrial pumps. Reinforced box-beam sections and column wrap protectors defend structural integrity against industrial material handling abuse.
E-Commerce & 3PL Hubs (Ardhiya & Al-Dajeej)
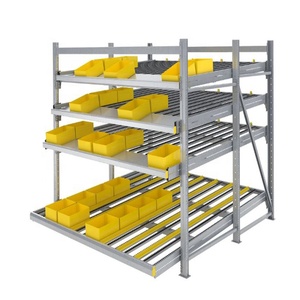
Agile selective picking layouts paired with Carton Flow tracks on lower levels and bulk back-to-back pallet storage on upper tiers. Optimizes both high-velocity piece picking and bulk replenishment throughput.
Market Strategic Intelligence
Macro Dynamics & Warehousing Trends in Kuwait (2025–2030)
The transformation of Kuwait’s supply chain landscape under New Kuwait Vision 2035 and its structural impact on industrial storage engineering.
Vertical Real Estate Optimization
Rising industrial land valuations in Shuwaikh and Mina Abdullah have pushed facility designs upward. Modern logistics builds regularly mandate clear ceiling heights of 11m to 14m. Back-to-back high-bay configurations allow operators to utilize structural height while maintaining structural stability through braced row-connector tying.
Transition to Semi-Automated & AMR Operations
To reduce human operating costs in high-temperature environments, Kuwaiti facilities are integrating Autonomous Mobile Robots (AMRs) and automated reach trucks. Modern back-to-back selective racks demand sub-millimeter manufacturing tolerances to guarantee sensor reflectance accuracy and automated fork alignment.
Stringent KFD Fire Safety Codification
The Kuwait Fire Department (KFD) strictly monitors longitudinal and transverse flue spaces in deep storage racking. Our back-to-back systems incorporate standardized engineered 150mm – 300mm row spacing gaps that align precisely with ceiling in-rack fire suppression nozzles, accelerating regulatory sign-offs.
Precision Factory Protocols
End-to-End Delivery Architecture: From Coil to Commissioning
Direct manufacturer execution eliminating intermediary markups, ensuring full steel batch traceability and turnkey compliance.
01
Structural Site Survey
Laser floor levelness profiling (DIN 18202 / TR34), concrete core strength validation, and localized column clearance modeling.
02
CAD & Finite Element Design
Simulation of full dead, live, and seismic loads using FEM software under strict adherence to Kuwait National Building Codes.
03
Precision CNC Roll-Forming
Continuous punching and automated multi-roll cold rolling of upright channels and interlocking box beams with zero gauge deviation.
04
Export Curing & Shipping
High-adhesion powder coating, rust-inhibiting seaworthy bundles, and direct oceanic container delivery to Shuwaikh / Shuaiba Ports.
05
Supervised On-Site Erection
Factory-certified installation, torque calibration of all anchor bolts, EN 15635 initial load testing, and load-capacity plaque certification.
Why Industrial Procurement Chooses Us
Manufacturer Strengths & Factory Engineering Superiority
Combining extensive steel fabrication capacity with global structural validation to deliver turnkey warehouse solutions in Kuwait.
Direct OEM / Factory Source
By eliminating trading intermediaries, we provide direct manufacturer pricing, agile engineering adjustments, and dedicated rolling schedules. Custom column profiles, heavy baseplates, and specialized paint colors (RAL specs) are handled entirely in-house.
Full EN 15512 Certification
Every beam-to-frame connector, safety lock pin, and upright splice undergoes rigorous structural mechanical testing. We supply mill test certificates (MTC), static load calculations, and comprehensive engineering documentation ready for municipality and civil defense approvals.
Turnkey Lifecycle Support
Our commitment extends beyond port delivery. We offer on-site engineering supervision, annual EN 15635 rack safety inspections, damage retrofit kits, and modular expansion sections ensuring your facility scales smoothly over decades.
Procurement & Technical Queries
Frequently Asked Questions by Kuwaiti Warehouse Developers
Practical guidance covering structural standards, civil defense compliance, delivery logistics, and ground-level installation parameters.
Why choose Back-to-Back Pallet Racking over single rows?
Single-row selective racking requires an operating aisle for every rack run. By connecting two single rows back-to-back via rigid tubular steel row spacers, you share forklift aisles across two sides. This configuration recovers up to 40% of building footprint volume while preserving 100% immediate selectivity for high-SKU inventory.
Does your racking comply with Kuwait Fire Department (KFD) rules?
Yes. KFD codes require clear vertical flue spaces between back-to-back pallets to permit unobstructed sprinkler water penetration. Our systems feature engineered row spacers (typically 150mm – 300mm wide) paired with backstop pallet stops to maintain these safety clearances permanently.
How does the steel coating resist Kuwait's coastal humidity and heat?
We apply an automated multi-stage pre-treatment, including zinc phosphating, followed by electrostatic deposition of high-polymer thermosetting polyester powder (70–90μm thickness) cured at 200°C. For coastal outdoor or open-canopy facilities in Mina Abdulla, hot-dip galvanized components are supplied to resist salt spray corrosion.
What are the typical sea-freight transit times to Kuwait ports?
Standard manufacturing takes 15 to 25 days depending on project tonnage. Oceanic container transit to Shuwaikh Port or Shuaiba Port generally requires 18 to 26 days. We provide end-to-end export documentation, including clean Bills of Lading, Legalized Certificates of Origin, and packing lists for smooth Kuwait Customs clearance.
What concrete floor specification is needed for heavy installations?
For racking heights of 6m to 12m with pallet loads of 1,000kg to 1,500kg, a reinforced concrete floor slab with a compressive strength of at least C25/C30 (25–30 N/mm²) and a minimum thickness of 180mm to 200mm is recommended. We run point-load calculations to size baseplates and select anchor bolts that prevent slab breakout.
Can our local Kuwaiti contractors handle the mechanical assembly?
Yes. We supply comprehensive installation shop drawings, assembly sequences, anchor torque specifications, and bolt schedules. Alternatively, we can dispatch seasoned factory installation supervisors to Kuwait to lead, align, and commission the setup on site.