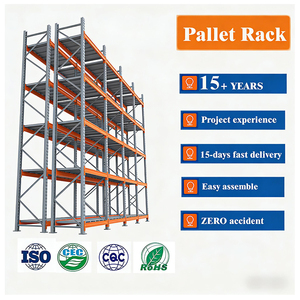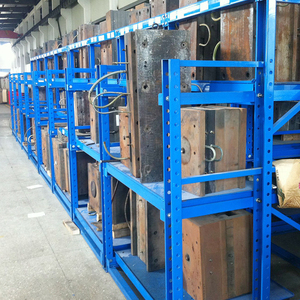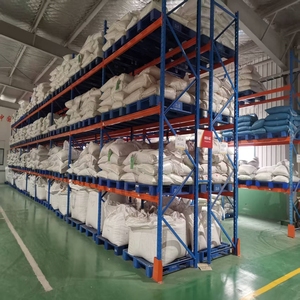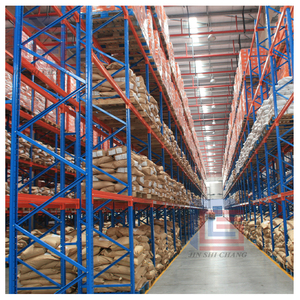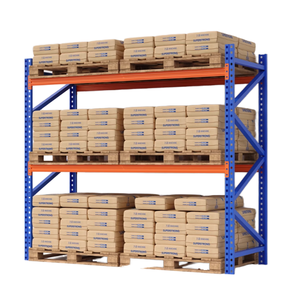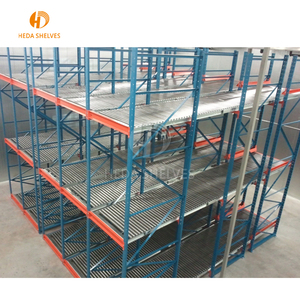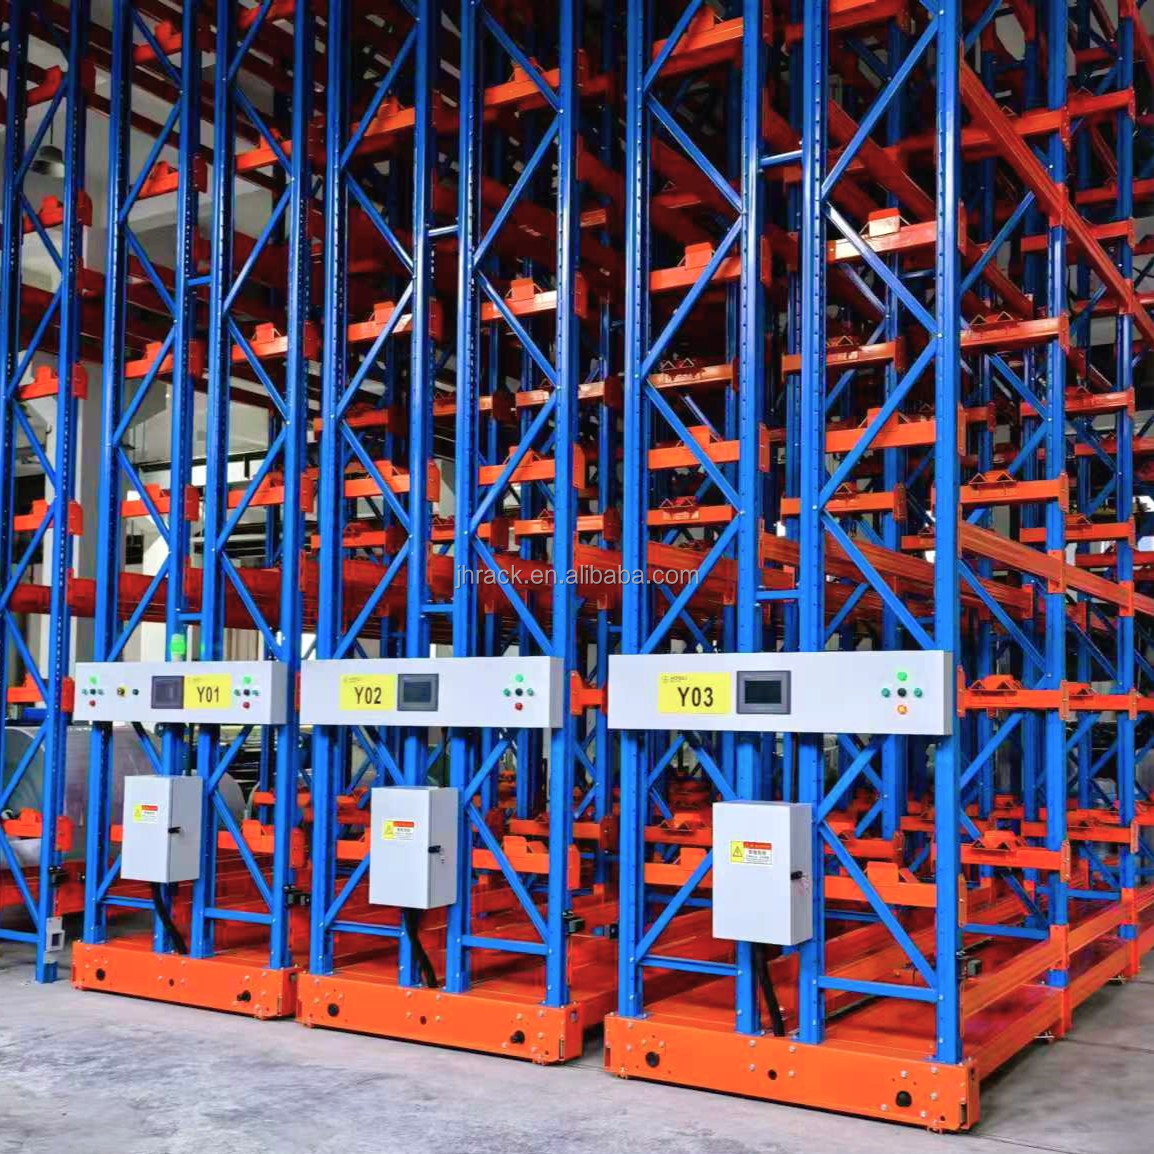
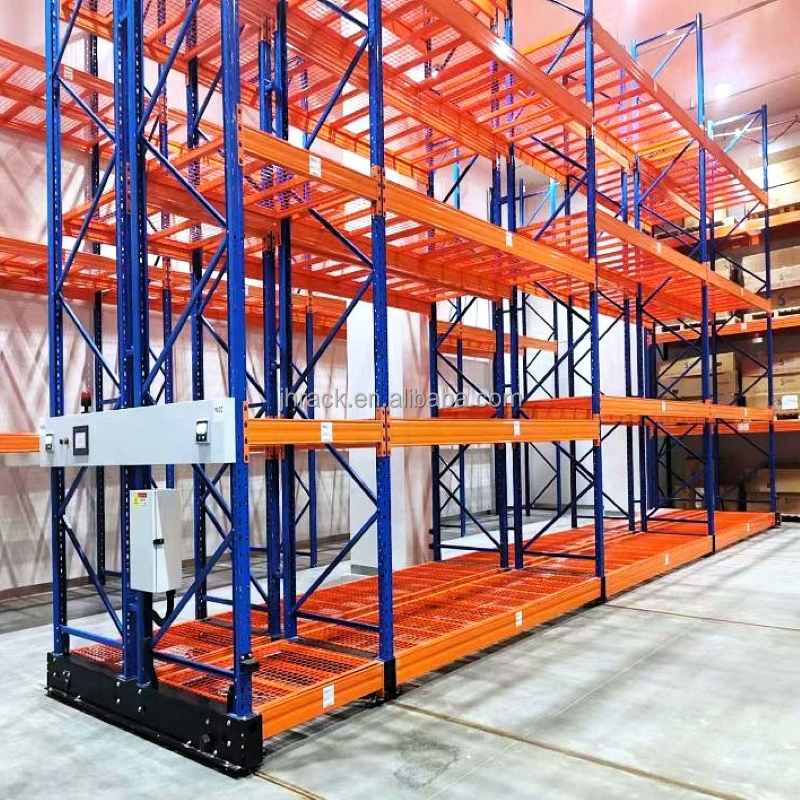
Industrial Heavy Duty High Efficiency Warehouse Electric Mobile Storage Shelf Automatic Mobile Racking System Pallet Rack
Product Description
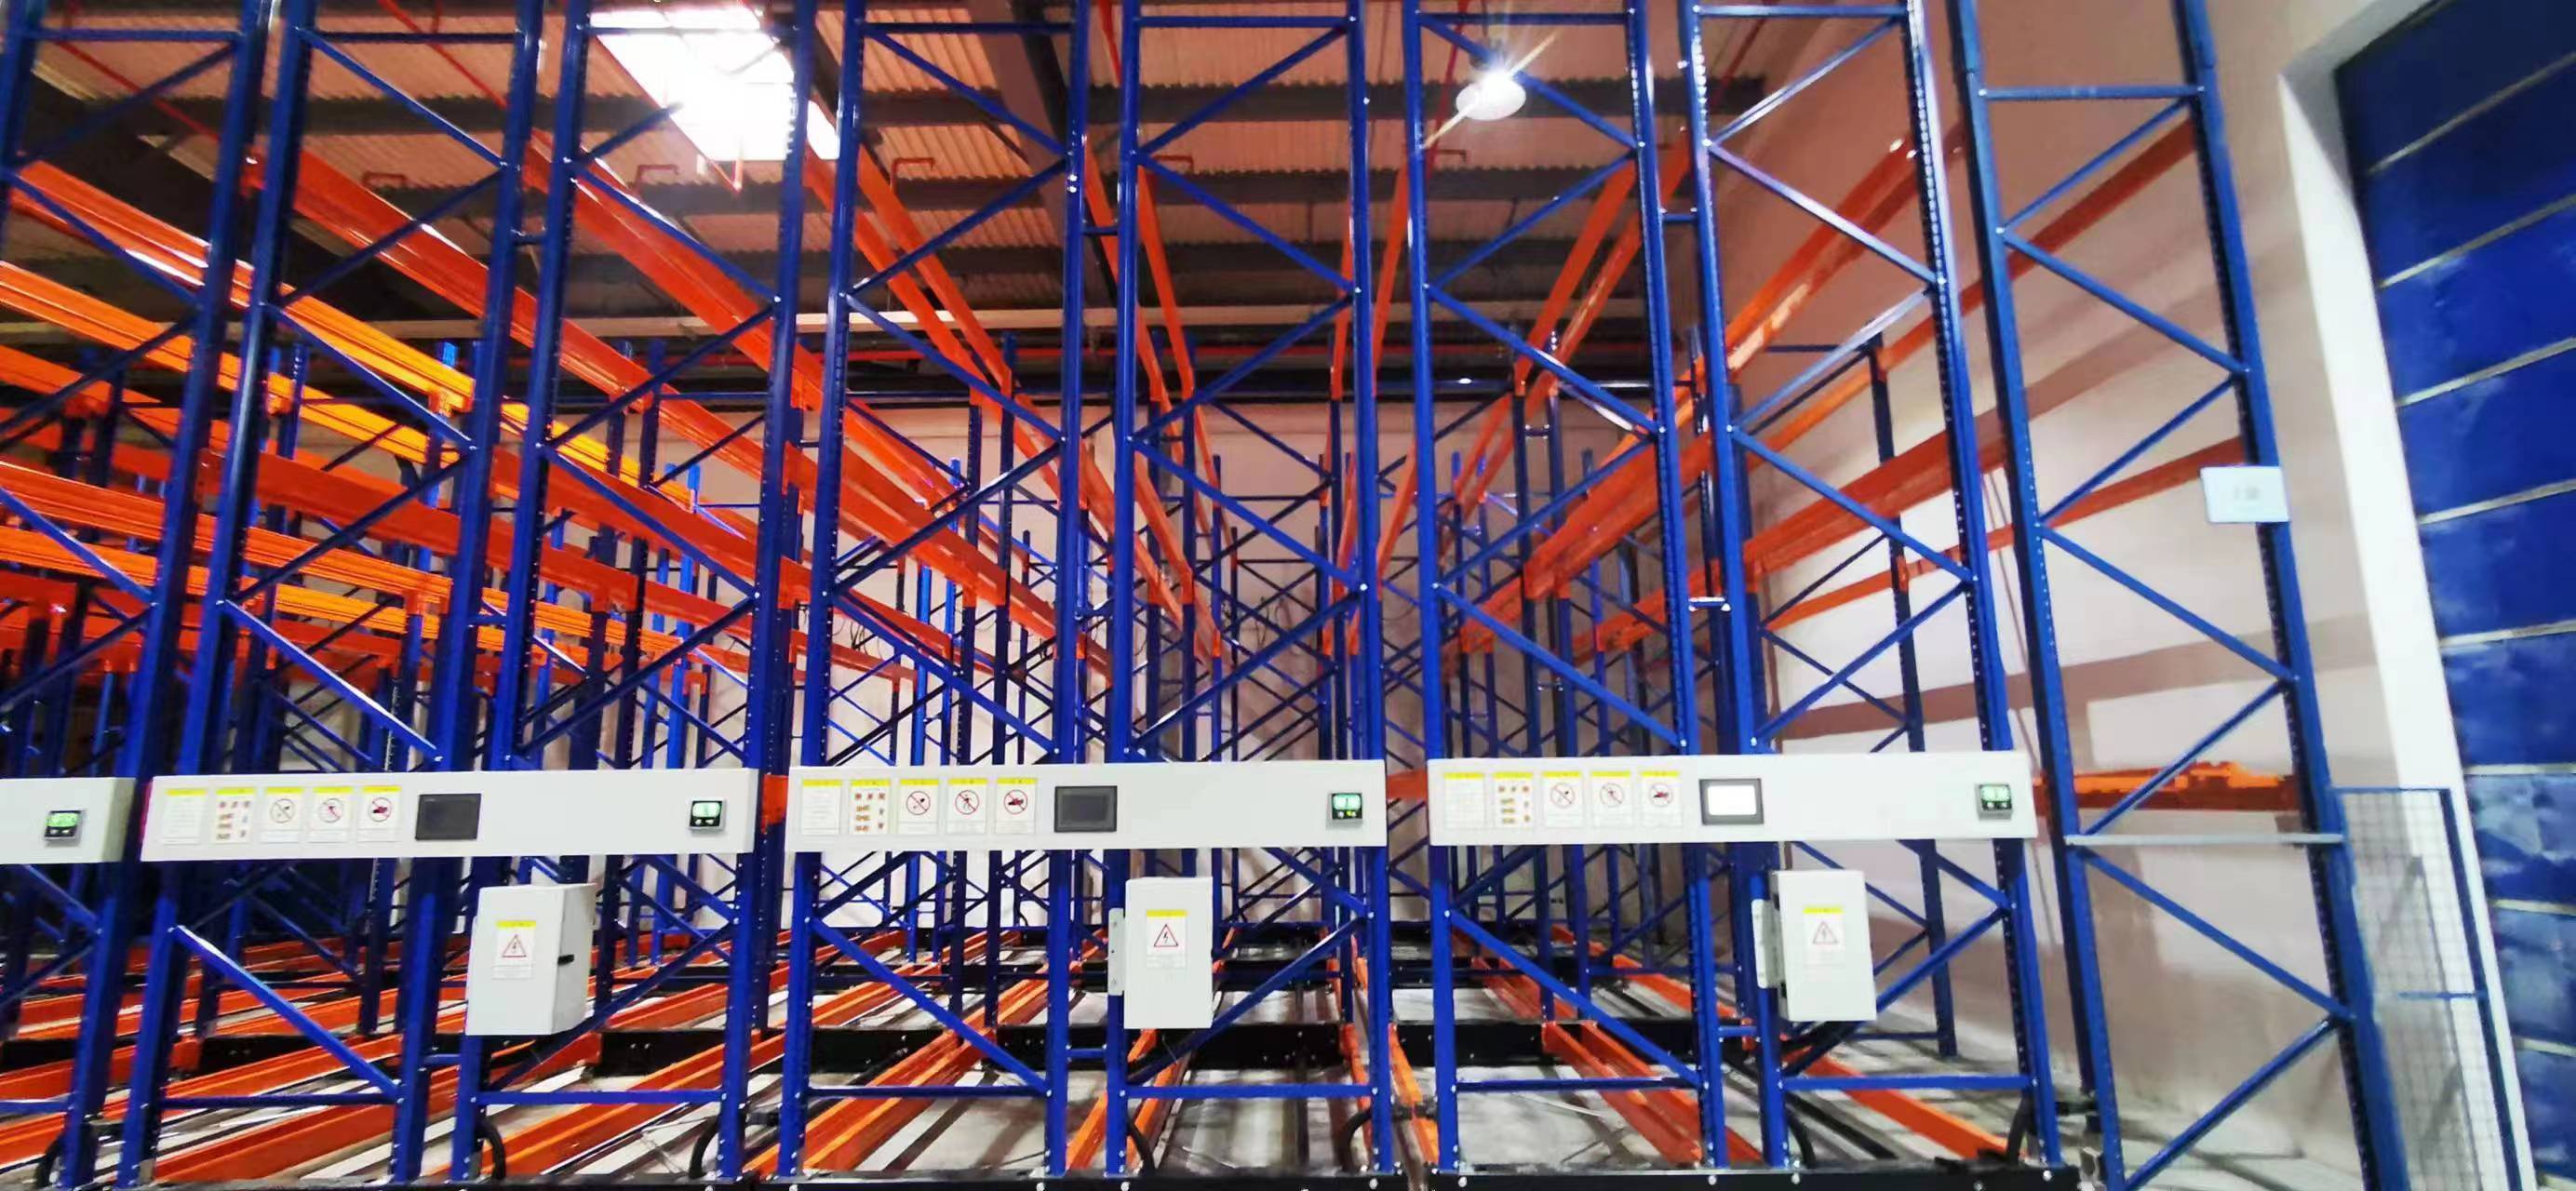
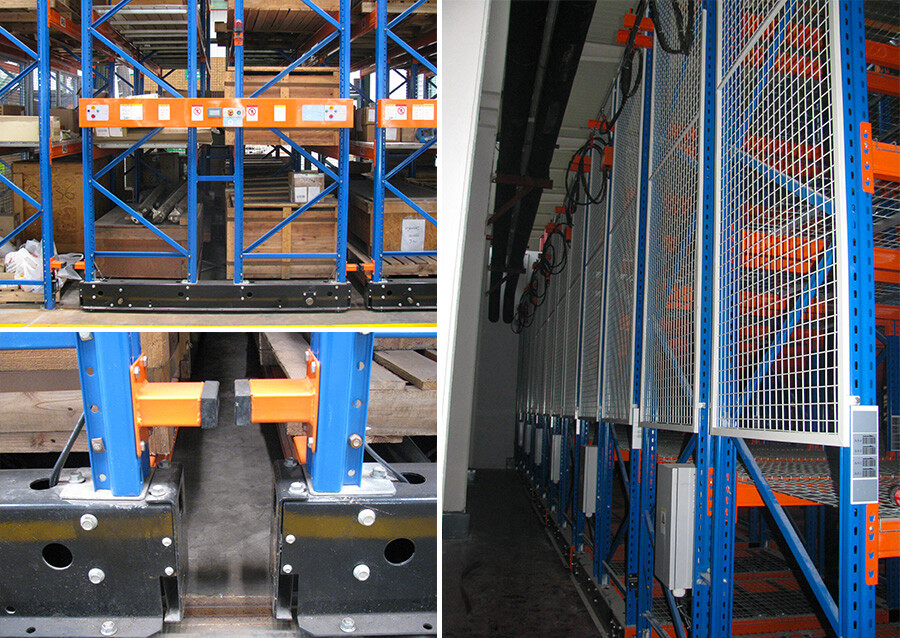
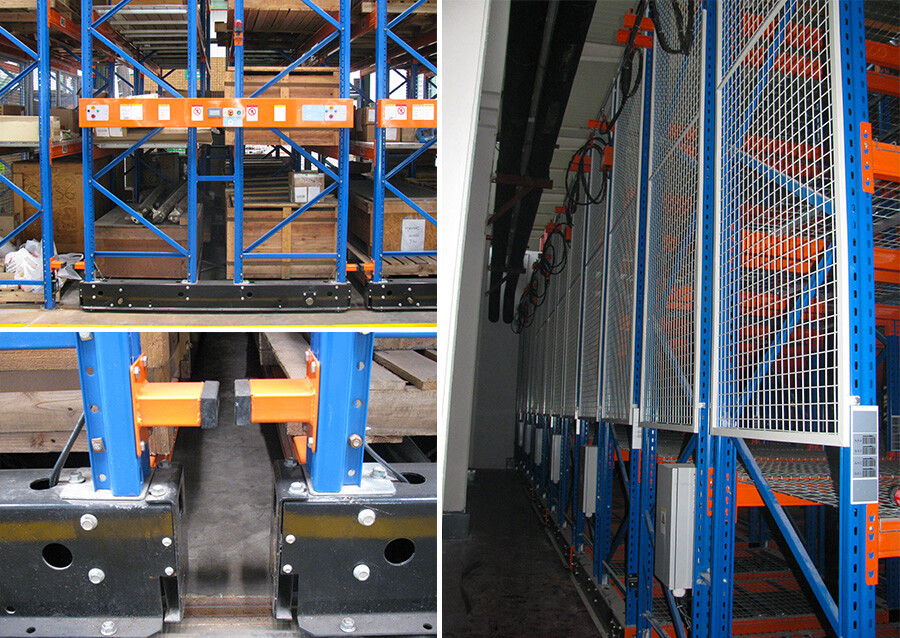
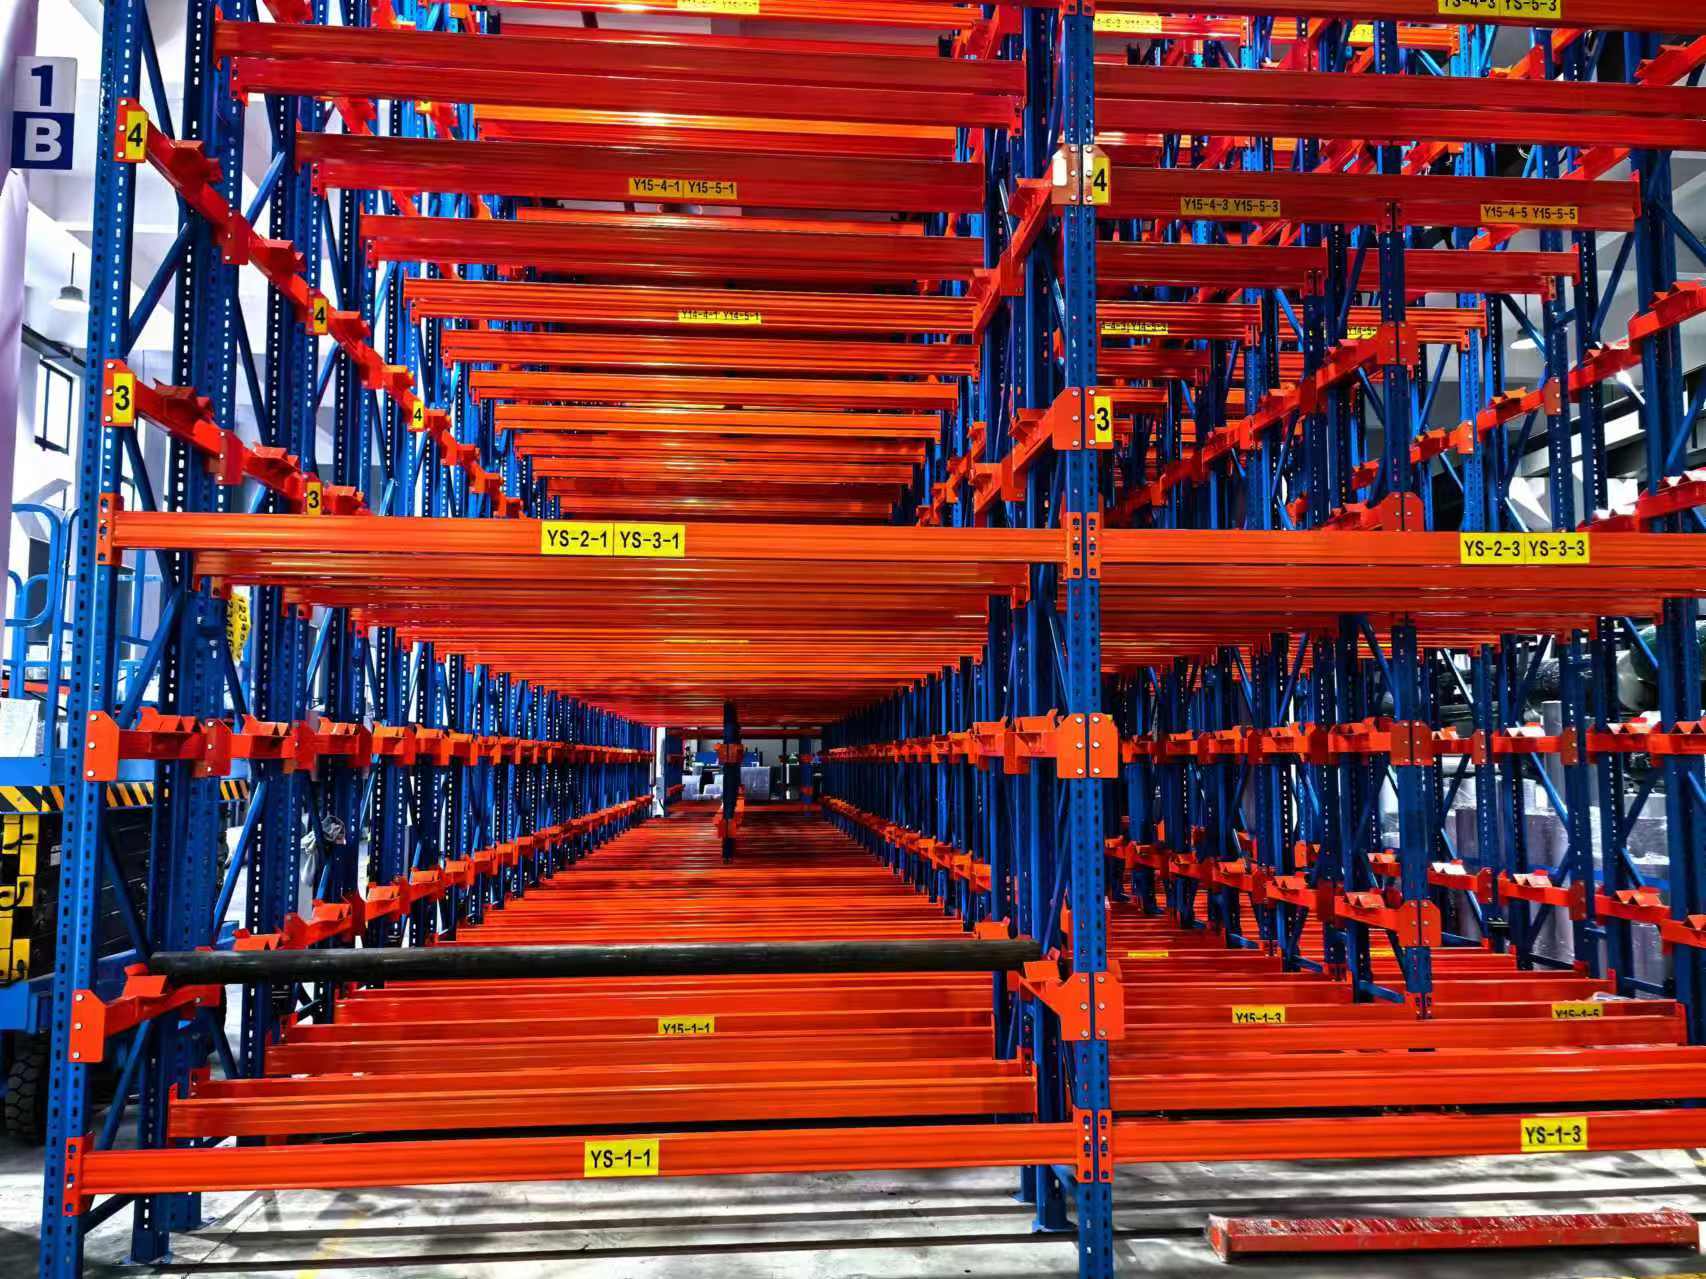
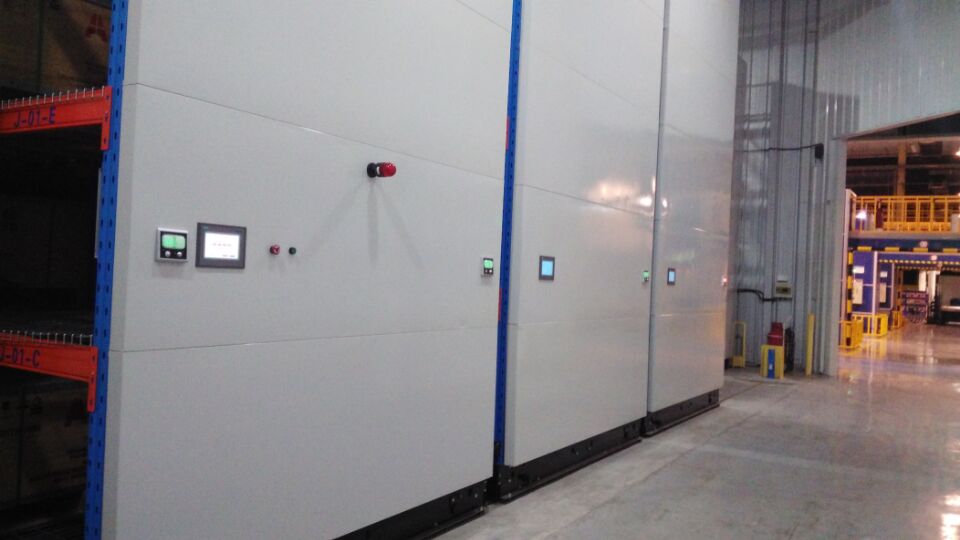
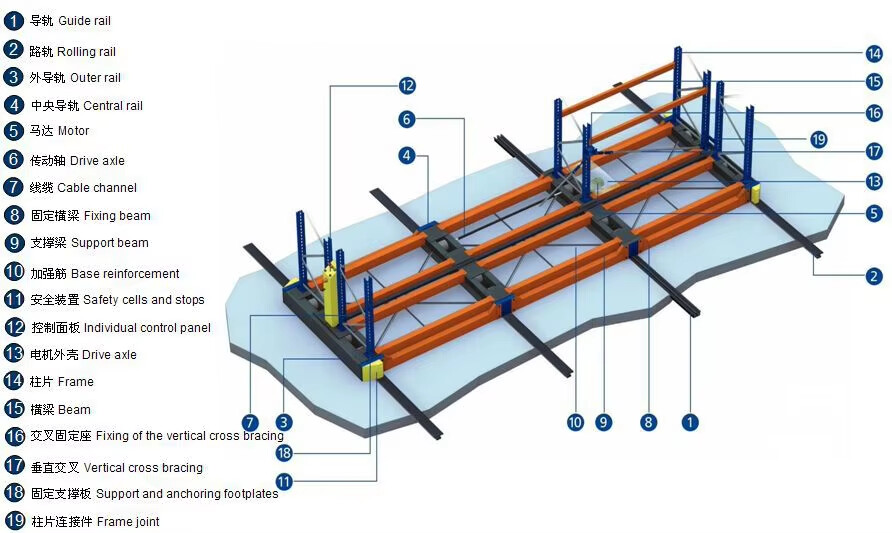
The Electric Mobile Racking System is a professional high-density intelligent warehousing solution integrating top-tier computer WMS warehouse management software, imported PLC systems, frequency inverters, precision sensors, 7-inch touch screens, Android intelligent handheld data collectors, and advanced RFID/bar code tracking technologies.
Engineered as a comprehensive, intelligent modern warehouse management infrastructure, the system requires only a single moving aisle for operations, dramatically increasing storage capacity and floor space utilization.
Product Display
Product Structure
Product Advantages
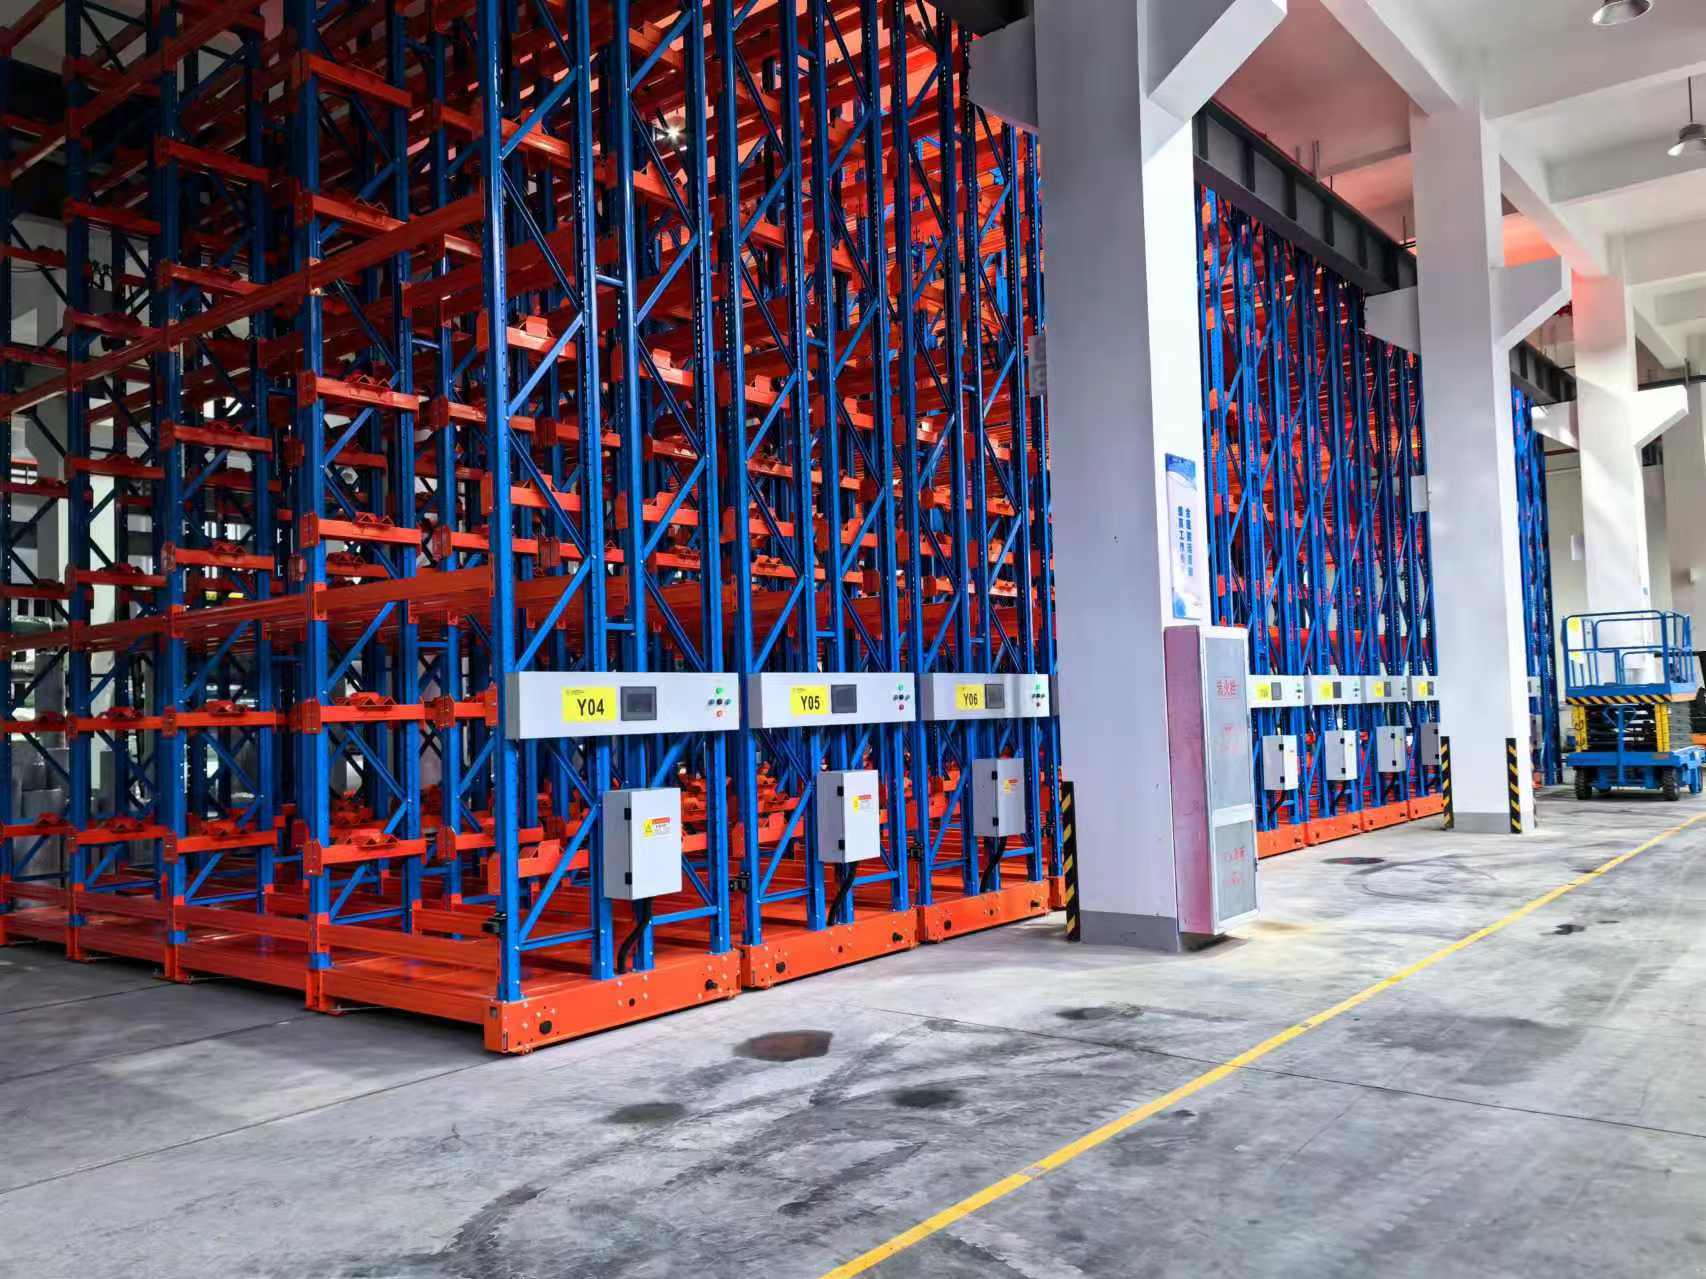
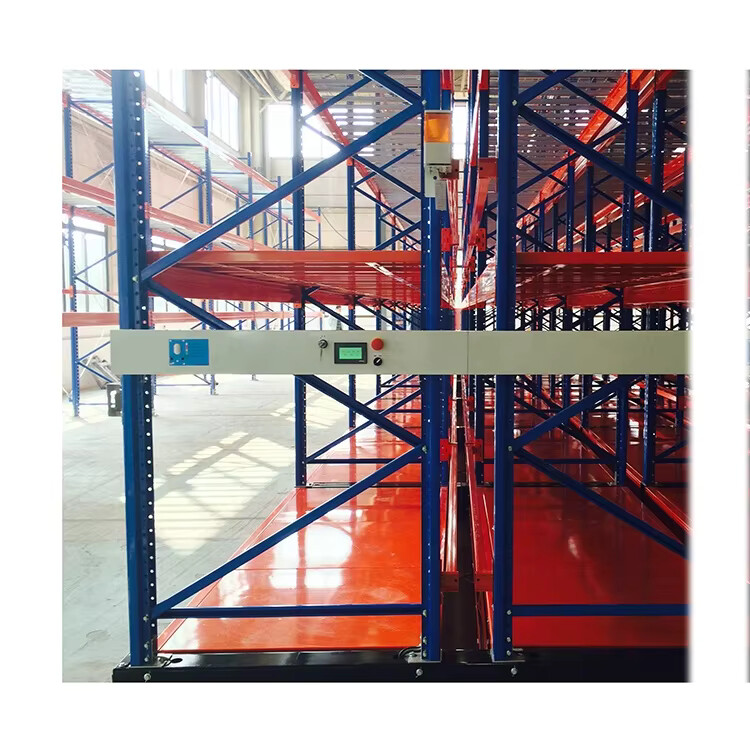
Specification
| Model | Load Capacity | Movement Speed | Motor Power | Power Supply Form | Power Supply | Control Mode | Safety Device |
|---|---|---|---|---|---|---|---|
| Railed | 32 tons / sets | Max. 10 M/min | Max. 1.5 KW | Tow cable synchro line | 220V / 380V | Automatic linkage / PC control / Remote control | Channel self-locking, Automatic detection, Emergency stop, Sound & light alarm, Overload & overcurrent protection |
| Trackless | 16 tons / sets |
Packing & Delivery
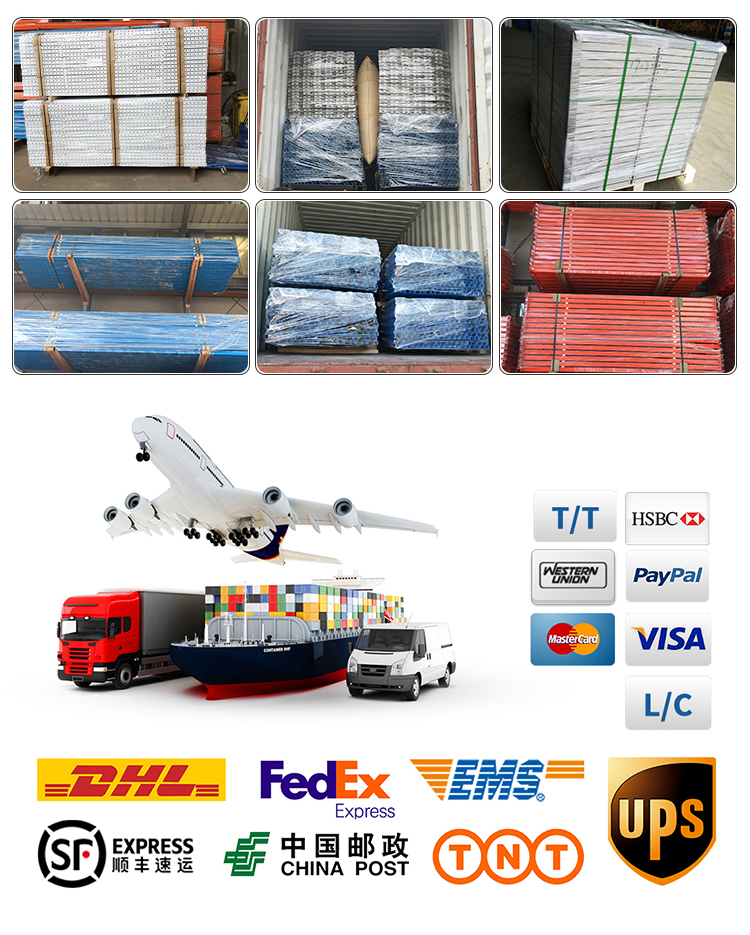
To better ensure the safety of your goods, professional, environmentally friendly, convenient, and efficient packaging services are provided with standardized protective wrapping.
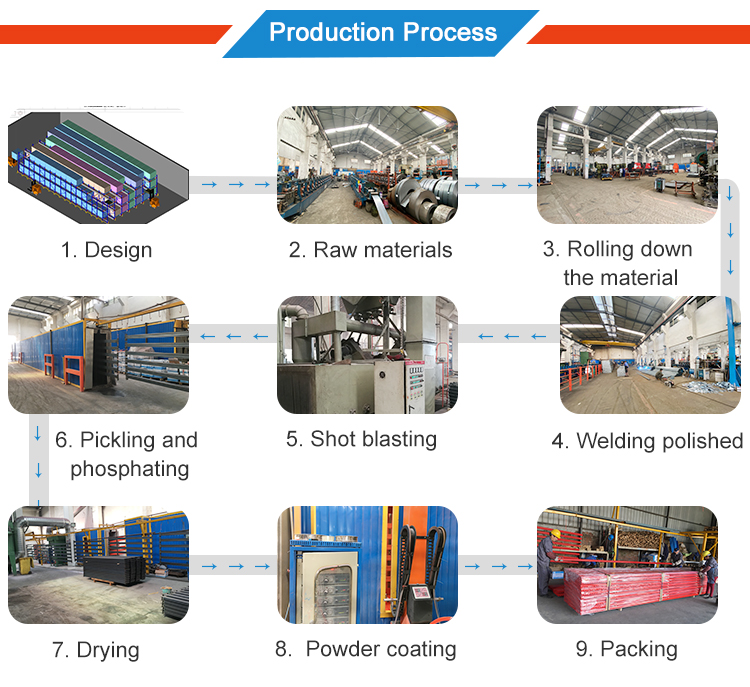
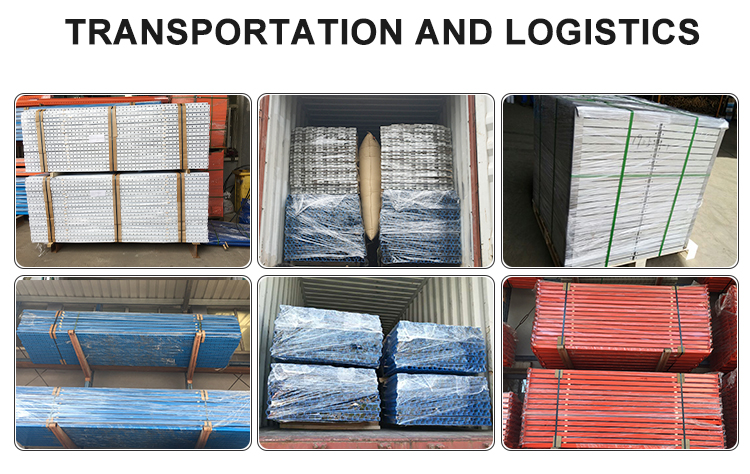
Company Profile
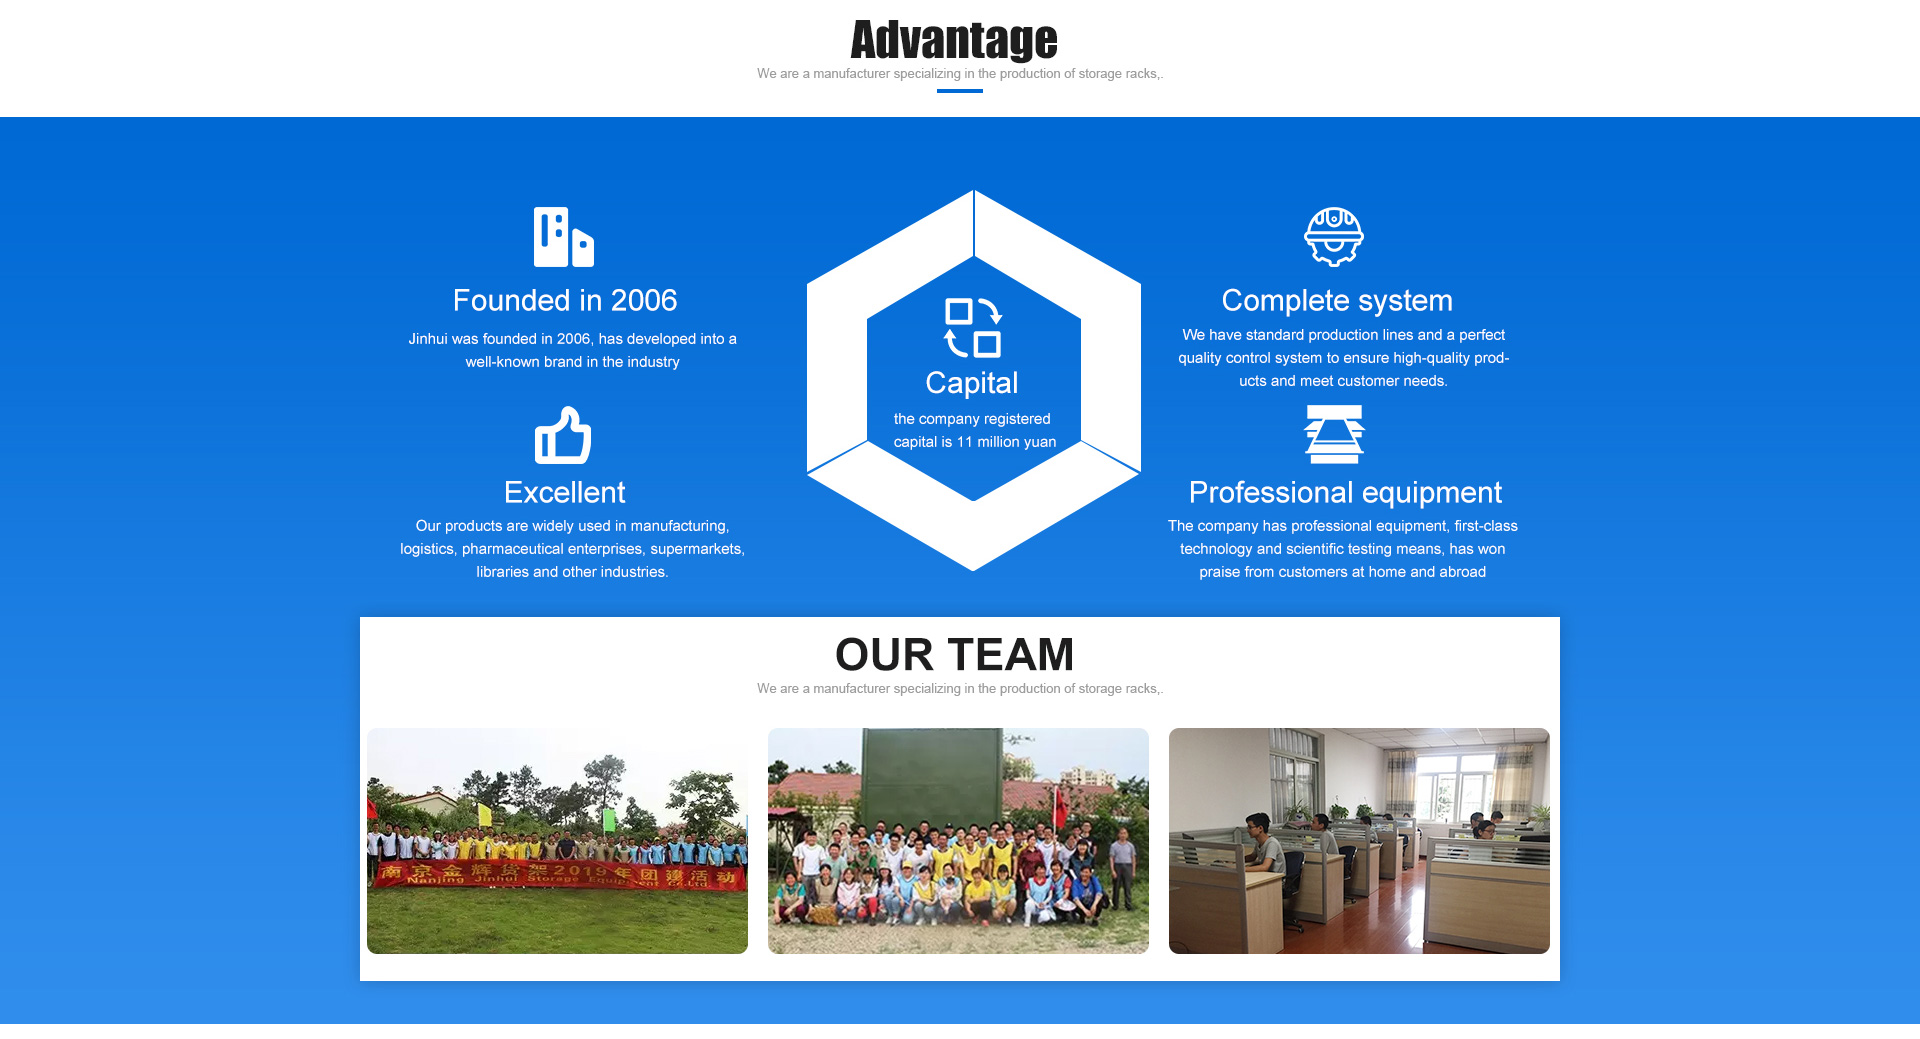
Nanjing Jinhui Storage Equipment Co., Ltd., established in 2006, is a premier enterprise engaged in the research, development, sale, and servicing of pallet racking, mezzanine floors, cantilever racking, light-to-medium shelving, and heavy-duty steel pallets.
Operating two production plants covering an expansive 40,000 square meters—comprising 20,000 m² of modern industrial workshops and 4,000 m² of corporate facilities—the company is situated in Nanjing with strategic transportation access.
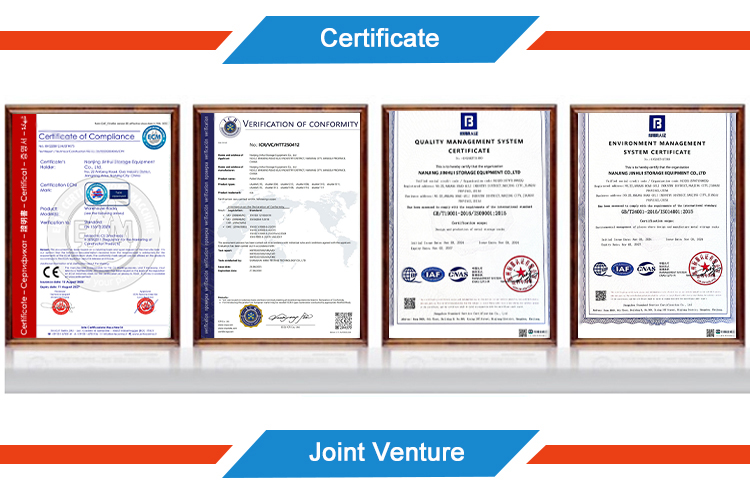
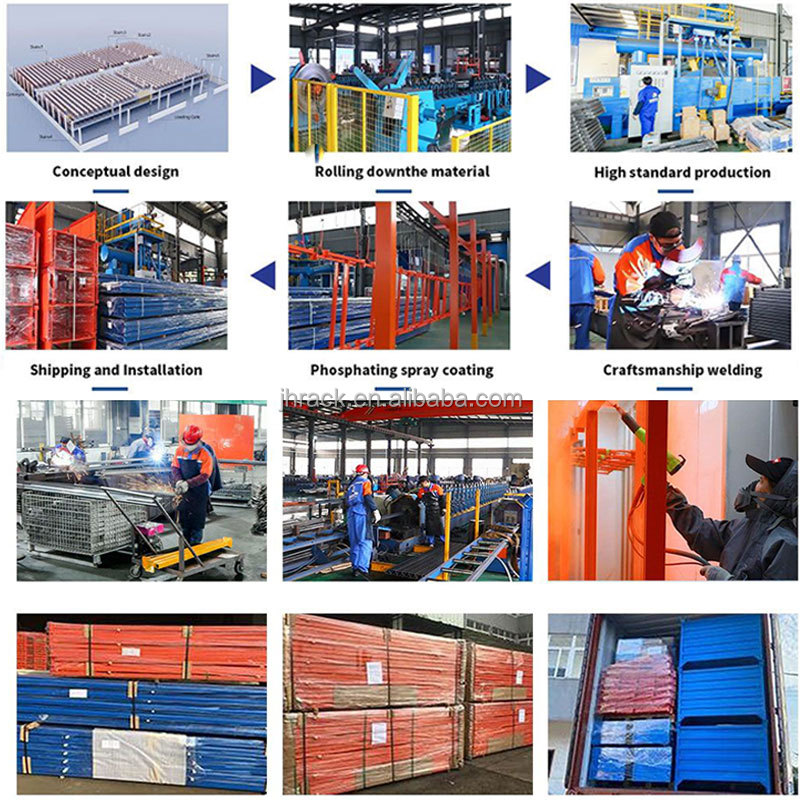
Backed by advanced automated production lines and skilled installation & after-sales teams, we adhere strictly to international quality control benchmarks. Nanjing Jinhui holds CE, ISO9001, ISO14001, and TUV certifications, supplying clients across Asia, North America, South America, and Africa, with comprehensive OEM and ODM capabilities.
Certificates & Global Cooperation